
Steel Pipes for Chemical & Petrochemical Plants
An engineering reference for buyers of chemical-process pipe — process units, sour and corrosive service, utility and offsite lines, and tank-farm transfer — with the material ladder, NACE sour-service rules, weld and test requirements that keep a plant compliant.
Where Piping Is the Process
One line list, one material ladder, one accountable supplier.
In a chemical or petrochemical plant, the piping is not infrastructure around the process — it is the process. Lines carry acids, solvents, caustics, hydrogen, chlorine and hydrocarbons at combinations of temperature and pressure that turn ordinary steel into a consumable. Material selection is governed by ASME B31.3 in the American world and EN 13480 in the European one, and the line list — not the market price — decides the material.
CREATEEL supplies the full material ladder from one mill group — carbon steel A106 / A333, Cr-Mo alloy A335 P11–P91, stainless A312 TP304L/316L, duplex and super duplex to EN 10216 equivalents — with the impact, hardness, IGC and PMI tests, NACE sour-service compliance and EN 10204 3.1/3.2 certificates a process specification calls for.
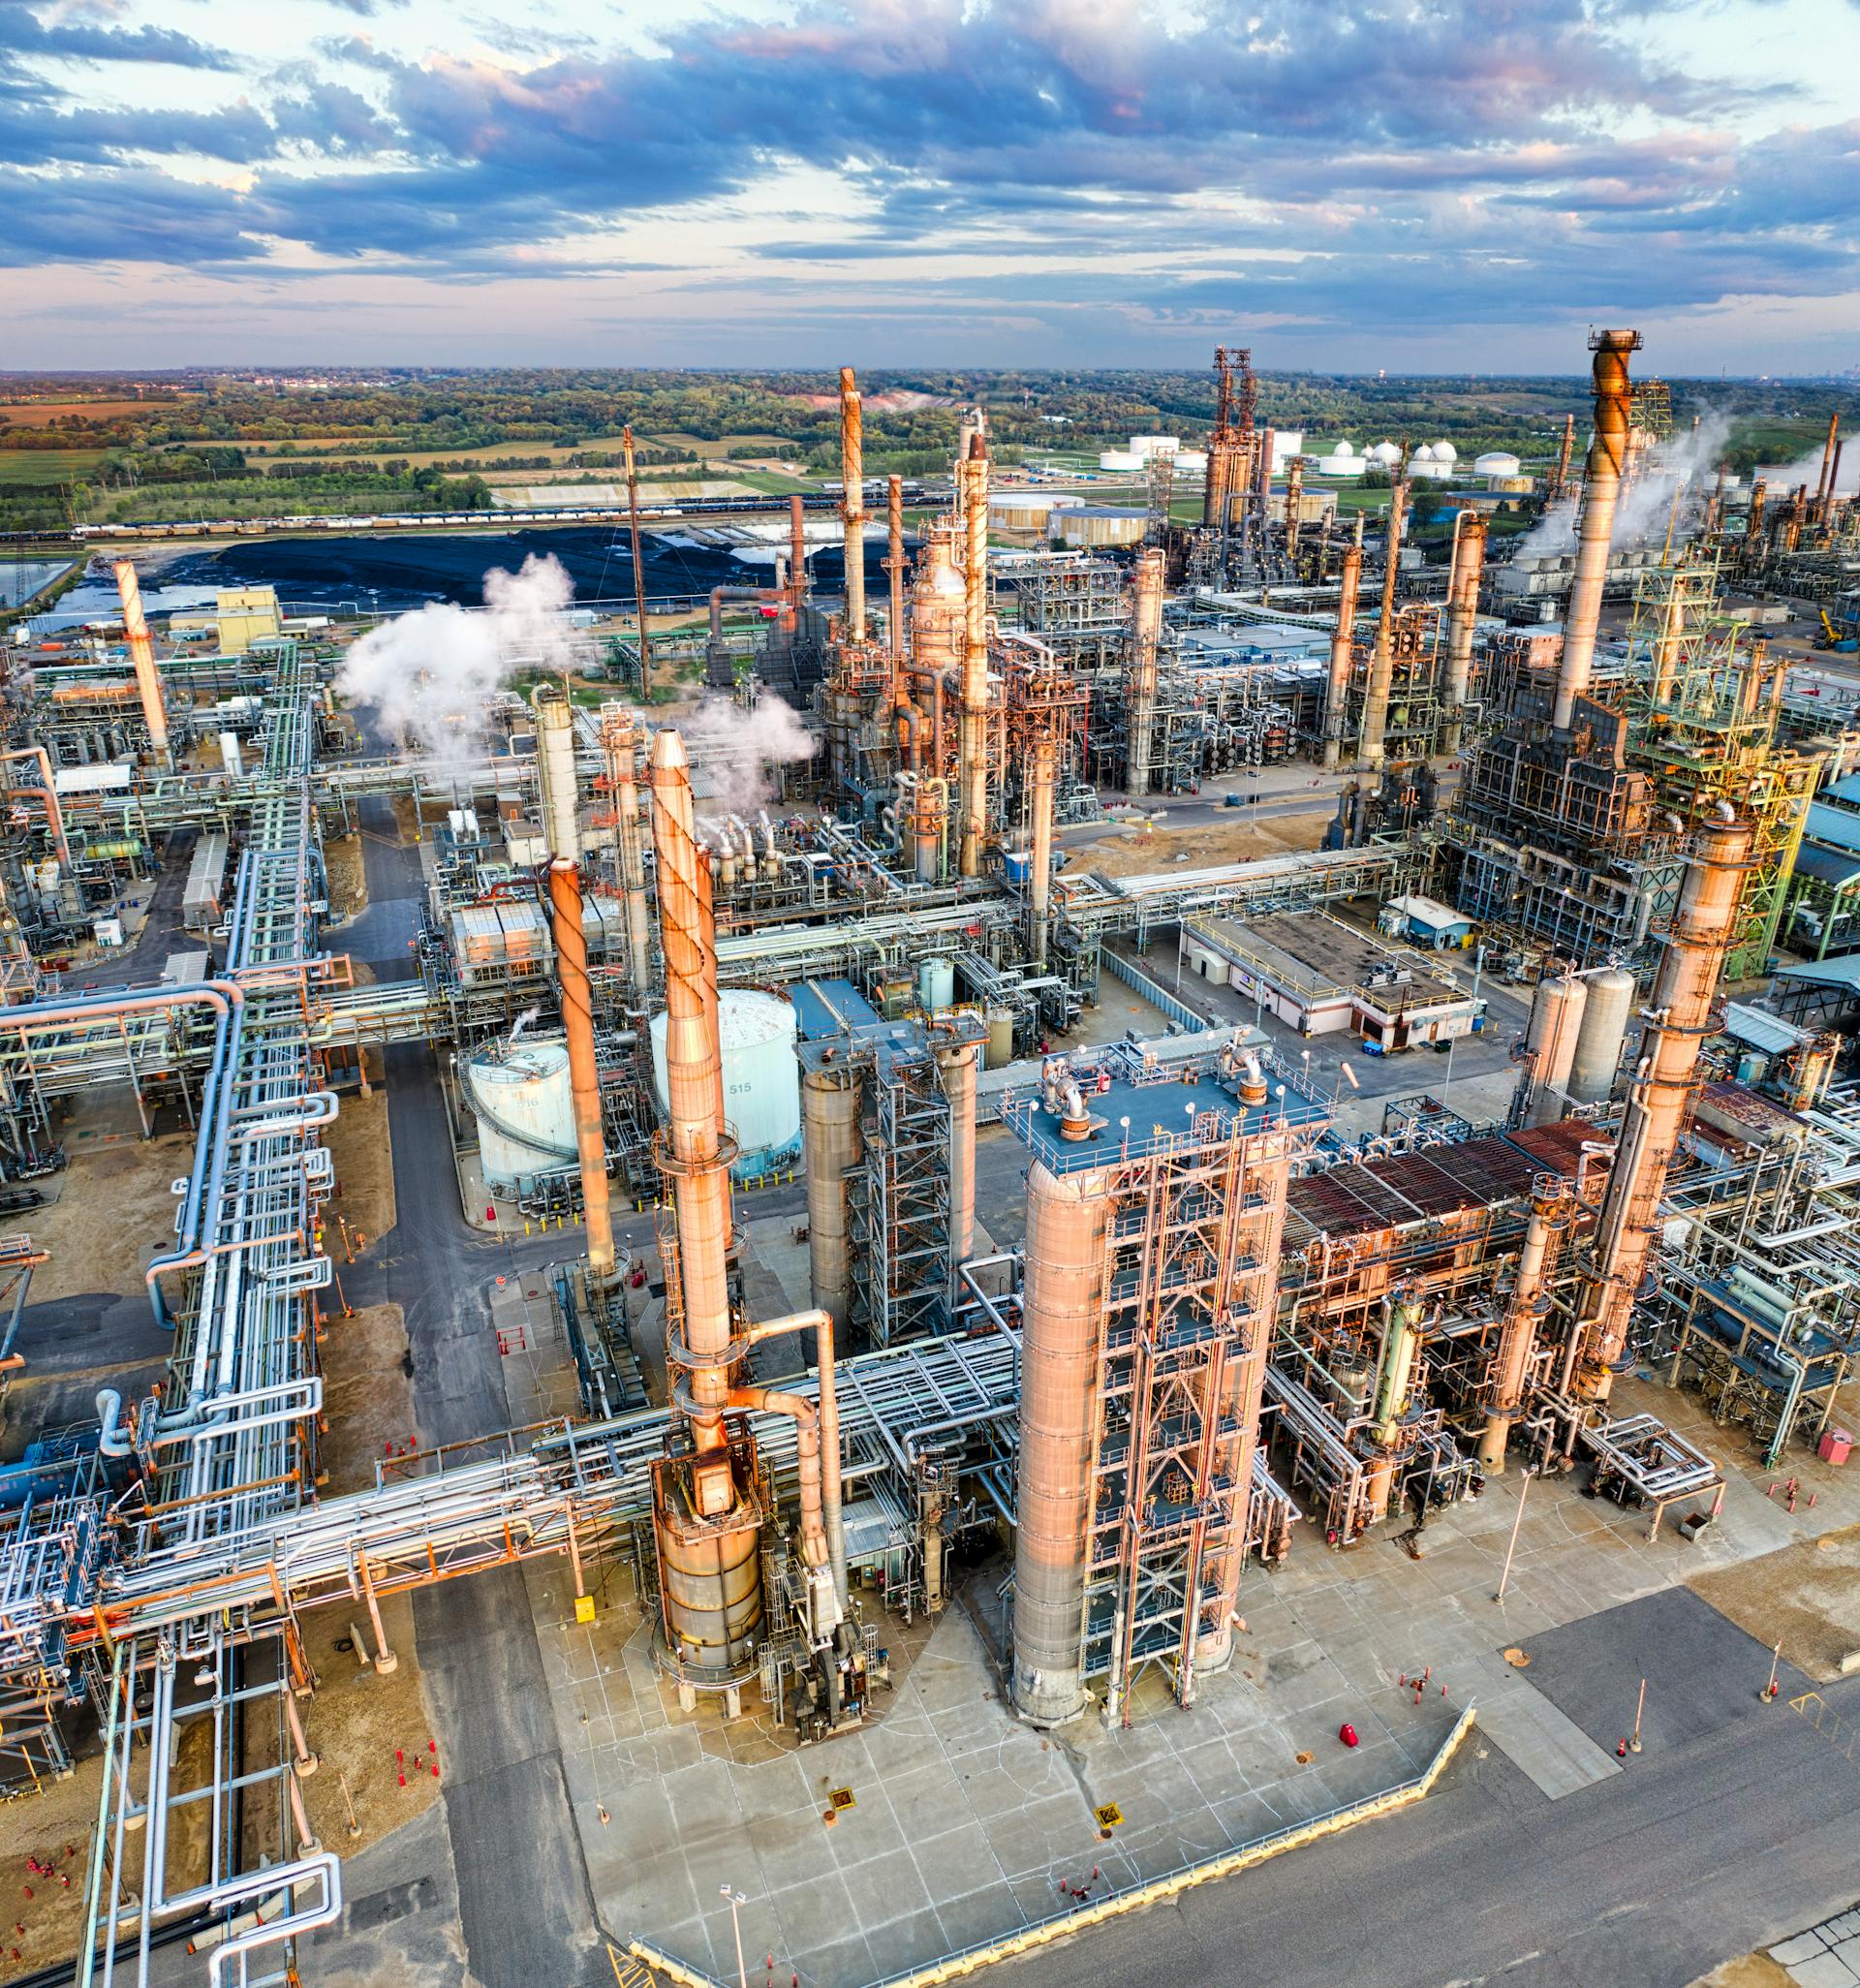
Process-plant rack: alloy and stainless lines on a single structure.
Four Forces That Decide a Chemical Pipe Spec
Chemistry, heat, sour service and paperwork — in that order.
Four forces decide every chemical-pipe spec. Get any one wrong and the line fails early — or the budget does. The rest of this page walks through how material class, chemistry, sour rules and testing answer each one.
Corrosive media
Acids, caustics, chlorides and solvents attack the wall from inside. The material ladder steps up in cost roughly two-fold per class — so over-specifying is expensive too.
- Key specifications
- • pH + chlorides decide
- • 316L where CS fails
- • Duplex where 316L fails
Temperature & hydrogen
Above ~425 °C carbon steel loses creep strength; hydrogen service adds Nelson-curve limits. Cr-Mo alloy (P11/P22/P91) carries hot hydrogen and steam headers.
- Key specifications
- • >425 °C = Cr-Mo
- • Nelson curves for H2
- • PWHT mandatory
Sour service (H2S)
Wet H2S triggers sulphide stress cracking. NACE MR0175 / ISO 15156 caps hardness at 22 HRC and prescribes HIC / SSC testing on qualified heats.
- Key specifications
- • ≤22 HRC cap
- • HIC per TM0284
- • SSC per TM0177
Documentation & traceability
Every heat must be traceable to its certificate, with the special tests the line list calls out — impact, hardness, IGC, PMI — and nothing the line does not need.
- Key specifications
- • EN 10204 3.1 / 3.2
- • PMI on alloy lines
- • Heat-number trace
Four Service Groups in Every Plant
Process, sour, utility and terminal — one supplier covers all.
From an ethylene cracker to a sulfuric-acid plant to a tank farm, the same four families appear — each pushing a different parameter to the front: temperature, chemistry, simplicity or size.
Four plant service groups
Every flowsheet runs the same four pipe families — this page covers all of them.
Where each pipe family fits
Click through to the detail cards below
Process units
Reactor feed, distillation, heat-exchanger circuits. The highest-temperature, highest-pressure lines on the plot — mostly A106 and A335 alloy.
- Key specifications
- • ASME B31.3 design
- • Seamless preferred
- • Corrosion allowance sized
Sour & corrosive
Wet H2S, acids and chloride brines. Material steps to 316L, duplex 2205 or nickel alloys under NACE MR0175 hardness control.
- Key specifications
- • ≤22 HRC steels
- • Duplex PRE≥35
- • HIC/SSC tested
Utility & offsite
Steam, condensate, cooling water, plant and instrument air. Carbon steel, galvanized or coated — simple specs, big quantities.
- Key specifications
- • A53 / A106 Gr.B
- • A333 for cold climate
- • Galvanized or painted
Storage & terminal
Tank-farm transfer, loading arms, product movement. Larger bore, lower pressure — ERW and LSAW with product-compatible coatings.
- Key specifications
- • ERW / LSAW >6 in
- • API-compatible coatings
- • Hydro per B31.3
The Material Ladder for Process Piping
Carbon → Cr-Mo → stainless → duplex → nickel — cost doubles per step.
Process engineers apply a simple shorthand: carbon steel wherever it survives with a sensible corrosion allowance; stainless 316L where chlorides or cleanliness rule out carbon; duplex where chlorides rule out 316L; nickel alloys where temperature plus chemistry rule out everything cheaper. Each step up roughly doubles material cost — a wrong line-list assumption is expensive in both directions.
The material ladder
Per ASME B31.3 / EN 13480 selection practice
Family selection table
Service, then watch-outs — the line list decides
| Material family | Typical service | Watch-outs |
|---|---|---|
| Carbon steel (A106 B/C, A333, P235GH–16Mo3) | Hydrocarbons, steam, air, most organics | Sulphidation in high-S streams; brittleness at low temp |
| Cr-Mo alloy (A335 P5/P9/P11/P22, 13CrMo4-5) | High-temp hydrogen, furnace transfers, steam headers | Hydrogen attack (Nelson curves); PWHT mandatory |
| Austenitic SS (A312 TP304L/316L, 1.4301/1.4404) | Corrosive chemicals, low temp, cleanliness | Chloride SCC above ~60 °C; use L grades; IGC tests |
| Duplex (A790 S31803/S32750, 1.4462/1.4410) | Seawater cooling, brine, aggressive liquor | Tight welding windows; verify ferrite and PREN |
| Nickel alloys (825 / 625 / C-276) | Acids, H2S-rich sour, deep-well chlorides | Cost — justify by life-cycle; long lead times |
Stainless, Duplex & PREN Selection
24 for mild duty, 35 for seawater, 40+ for hot brine.
Pitting resistance is the yardstick for chloride service. PREN = %Cr + 3.3×%Mo + 16×%N: TP316L sits at 24, fine for mild chemical duty but not seawater; duplex 2205 (PRE≥35) delivers roughly twice the proof strength of austenitic grades and resists chloride and H2S stress-corrosion cracking; super duplex 2507 (PRE≥40) takes brine and aggressive process liquor. Austenitic grades need the L (low-carbon) suffix for welded service to avoid sensitisation, and chloride SCC is a real risk above ~60 °C — that is where duplex earns its premium.
Pitting resistance (PREN)
Higher PREN = more chloride resistance before pitting starts.
Alloy selection table
Yield values per ASTM / EN; duplex wins on strength too
| Grade | Standard | Fy min (MPa) | Best for |
|---|---|---|---|
| TP304L | ASTM A312 / EN 1.4307 | 170 | General corrosion, low temp, cleanliness |
| TP316L | ASTM A312 / EN 1.4404 | 170 | Mild chlorides, acids, pharma-grade |
| Duplex 2205 | ASTM A790 S31803 / 1.4462 | 450 | Seawater cooling, brine, sour |
| Super Duplex 2507 | ASTM A790 S32750 / 1.4410 | 550 | Hot brine, aggressive liquor |
| Alloy 825 | ASTM B423 N08825 | 240 | Sulfuric / phosphoric acid service |
| Grade | Nominal chemistry | PREN | Typical duty |
|---|---|---|---|
| TP 304L | 18 Cr – 8 Ni – low C | ≈ 18 | Mild process and utility lines |
| TP 316L | 16 Cr – 10 Ni – 2 Mo – low C | ≈ 24 | Chloride-bearing duties, coastal plants |
| 2205 duplex | 22 Cr – 5 Ni – 3 Mo – 0.17 N | ≈ 35 | Seawater cooling, high-chloride brines |
| 2507 super duplex | 25 Cr – 7 Ni – 4 Mo – 0.27 N | ≥ 40 | Hot seawater, aggressive brines |
Note: PREN ranks resistance, it does not guarantee it — crevice geometry, temperature and pH decide whether pitting starts. The “L” in 304L/316L caps carbon below ≈ 0.03% so welds stay free of sensitisation without full solution annealing, which is what the intergranular tests in our QA section verify.
Sour Service: NACE MR0175 / ISO 15156
Wet H2S caps hardness at 22 HRC and demands tested heats.
Where the medium contains wet H2S, the environment is sour and the rules harden immediately. NACE MR0175 / ISO 15156 restricts hardness (≤22 HRC for carbon steel), limits strength levels and prescribes test regimes to prevent sulphide stress cracking (SSC) and hydrogen-induced cracking (HIC). Compliance is condition-dependent, not a stamp: specify it with the actual H2S partial pressure and pH from the line list, and expect HIC testing per NACE TM0284 (CLR/CSR/CTR limits) and SSC testing per NACE TM0177 on qualified heats.
Sour-service qualification flow
From line list to tested, documented heat.
Sour-service requirements
Hardness, HIC, SSC and CRA routes
| Requirement | Limit / test | Standard |
|---|---|---|
| Hardness cap (carbon steel) | ≤ 22 HRC (≤ 248 HV) | NACE MR0175 / ISO 15156 |
| HIC acceptance | CLR / CSR / CTR limits on tested heat | NACE TM0284 |
| SSC qualification | Threshold stress on qualified heat | NACE TM0177 Method A |
| Sour-service CS pipe | Restricted chemistry + HIC-tested | ASTM A106 / API 5L + MR0175 |
| CRA alternatives | Duplex / nickel alloys in CRAs tables | ISO 15156-3 |
Steel Grades for Chemical & Petrochemical Pipe
A106 for the base load, A335 for the heat, A312/A790 for chemistry.
A106 Gr.B is the plant workhorse; A333 Gr.6 covers cold climates and refrigerated service; the A335 P-series steps up with temperature — P11 and P22 for steam and hydrogen, P91 where wall weight matters at the hottest headers. Stainless and duplex take over where chemistry, not heat, is the enemy. Temperature limits above are approximate design bands; creep checks govern the final call.
Temperature capability by grade
Where Cr-Mo alloy is required above ~425 °C.
Grade selection table
ASTM A106/A333/A335/A312/A790 · EN 10216
| Grade | Standard | Fy min (MPa) | Typical plant use |
|---|---|---|---|
| A106 Gr.B | ASTM A106 (SMLS) | 240 | Process lines, steam, hot hydrocarbons |
| A106 Gr.C | ASTM A106 (SMLS) | 275 | Higher-pressure process service |
| A333 Gr.6 | ASTM A333 | 240 | Low-temperature lines to -46 °C |
| A335 P11 | ASTM A335 (1.25Cr-0.5Mo) | 205 | Steam headers to ~550 °C |
| A335 P22 | ASTM A335 (2.25Cr-1Mo) | 205 | Hot hydrogen, furnace transfers to ~575 °C |
| A335 P91 | ASTM A335 (9Cr-1Mo-V) | 415 | High-temp headers to ~625 °C |
| TP316L | ASTM A312 | 170 | Corrosive chemicals, cleanliness |
| Duplex 2205 | ASTM A790 S31803 | 450 | High chloride, sour, seawater |
| EN 10216-2 P235GH | EN 10216-2 | 235 | European pressure piping |
| 16Mo3 / 13CrMo4-5 | EN 10216-2 | 280 / 290 | European Cr-Mo equivalents |
Wall Thickness & Corrosion Allowance
Pressure wall from the code; allowance from the chemistry.
Pressure wall comes from the code formula (B31.3: t = P·D / 2(SE+PY)); the engineering decision is the corrosion allowance added on top. Mild hydrocarbon service typically carries 1.5–3 mm; sulphidic crude units 3–6 mm; acidic or chloride services may get lining or an alloy jump instead of more wall. Wall loss is monitored by UT thickness survey, and the allowance defines the inspection interval — so it is a life-cycle number, not a fudge factor.
Allowance by service
UT thickness surveys turn allowance into an inspection interval
| Service | Typical allowance | Rationale |
|---|---|---|
| Mild hydrocarbon / utilities | 1.5–3 mm | Slow, uniform general corrosion |
| Sulphidic crude / high-S | 3–6 mm | Sulphidation scales with S content |
| Acid / chloride service | Alloy or lining instead | Allowance cannot outrun pitting |
| Caustic (>50 °C) | CS + PWHT or alloy | Caustic embrittlement risk |
| Monitored critical lines | Per RBI programme | Risk-based inspection sets interval |
Weldability, Preheat & PWHT
Alloy pipe succeeds or fails at the weld — control it.
Welding is where alloy pipe succeeds or fails. Carbon steel needs only a qualified procedure (ASME Section IX); Cr-Mo alloys add mandatory preheat and post-weld heat treatment (PWHT) with hardness surveys to catch untempered martensite; duplex demands tight heat-input windows and nitrogen purging to hold ferrite balance; stainless needs the right filler and interpass control to avoid sensitisation. Positive material identification (PMI) on alloy lines catches the catastrophic mistake — carbon installed where chrome was specified.
Welding & verification matrix
Per ASME IX / B31.3 and API practice
| Family | Welding requirement | Verification |
|---|---|---|
| Carbon steel (A106/A333) | Qualified WPS per ASME IX | Visual, RT/UT per B31.3 |
| Cr-Mo (A335 P11-P91) | Preheat + PWHT mandatory | Hardness survey after PWHT |
| Austenitic (A312) | L-grade filler, low interpass | IGC test where specified |
| Duplex (A790) | Heat-input window + N2 purge | Ferrite count, corrosion test |
| All alloy lines | PMI on installed welds | XRF / OES 100% or sample |
What ships from the mill
Ready for site welding without surprises
- • Bevelled ends, caps on both ends
- • WPS/PQR packages on request
- • PWHT + hardness certificates for alloy
- • PMI records for every alloy heat
CUI Awareness & External Protection
Under insulation, the coating is the pipe’s life insurance.
External protection in a plant is about insulation, not soil. The dominant failure mode is CUI — corrosion under insulation: water ingress into lagging turns insulated carbon-steel lines into hidden rust traps between 50 and 175 °C. Countermeasures: thermal-spray aluminium or high-build epoxy under insulation, sealed cladding, inspection ports. Where pipe is buried or exposed, FBE and 3PE coatings apply as usual. Internally, lining follows the chemistry — cement, epoxy or none, per the corrosion study.
External protection matrix
CUI is the plant killer — coat under insulation
| Condition | Protection | Standard / practice |
|---|---|---|
| Insulated CS, 50–175 °C | TSA or high-build epoxy + sealed cladding | CUI practice (API 583) |
| Insulated austenitic | Low-chloride insulation + coating | Avoid ESC from insulation |
| Buried / underground | FBE 300–450 µm / 3PE | ISO 21809 / AWWA C213 |
| Exposed atmospheric | Epoxy + PU topcoat (C5) | ISO 12944 |
| Acid internal service | Rubber / PTFE / glass lining | Per corrosion study |
CUI risk window
Why the 50–175 °C band needs special care
- • Water ingress + warm wall = fast rust
- • Hidden until insulation is stripped
- • Austenitic grades risk external chloride SCC
- • Inspection ports + coating = cheap insurance
Design Codes & Standard Stacks
B31.3 / EN 13480 for design, NACE for sour, PED for CE.
Chemical piping is governed by a stack of codes. ASME B31.3 is the process-piping design code in the American world; EN 13480 is the European metallic industrial piping code, with the Pressure Equipment Directive (PED 2014/68/EU) above it for pressure-bearing items in the EU. NACE MR0175 / ISO 15156 governs sour service, API 583 covers CUI management, and welding qualification follows ASME Section IX / ISO 15614. Material standards (A106, A335, A312, A790, EN 10216) sit underneath.
Common code stacks
Pick the region first, the code second
| Code | Scope |
|---|---|
| ASME B31.3 | Process piping design, fabrication, test |
| EN 13480 | Metallic industrial piping (EU) |
| PED 2014/68/EU | Pressure equipment directive, CE marking |
| NACE MR0175 / ISO 15156 | Sour (H2S) service material limits |
| API 583 | Corrosion under insulation management |
| ASME IX / ISO 15614 | Welding procedure qualification |
| ISO 12944 / API 583 | Atmospheric corrosion & CUI practice |
Standards flow
Product → design → protect → verify
A Six-Step Specification Guide
From line list to test certificate — the spec the mill needs.
Read the line list
Service, temperature, pressure, H2S partial pressure and pH — the line list, not price, decides the material.
Pick the material class
Carbon steel wherever it survives; 316L for chlorides; duplex for seawater; nickel for the extreme.
Set wall & allowance
B31.3 pressure wall, then corrosion allowance by chemistry — or lining / alloy jump instead.
Choose process & OD
Seamless for critical / small bore, ERW for utility, LSAW for large bore — per line class.
Handle sour & weld rules
NACE MR0175 hardness + HIC/SSC tests; preheat and PWHT for Cr-Mo; PMI for alloys.
Confirm tests & docs
Impact, IGC, PMI as called out; hydro per B31.3; EN 10204 3.1 (3.2 on request) with heat trace.
Quality Assurance: What We Test, and Why
Every line on the MTC ties back to a clause in the spec.
Chemical analysis
Heat & product analysis: C, Mn, S, P, Cr, Mo, Ni per grade
- Key specifications
- • ASTM A751 / EN 10204
Tensile & yield
Yield, tensile, elongation on transverse specimens
- Key specifications
- • ASTM A370 / EN ISO 6892-1
Impact (where called)
Charpy at line minimum temperature; A333 to -46 °C
- Key specifications
- • ASTM A370 / EN ISO 148
Hardness (sour)
≤22 HRC cap verified on sour-service heats
- Key specifications
- • NACE MR0175 / ISO 15156
HIC / SSC (sour)
CLR / CSR / CTR per TM0284; SSC per TM0177 on qualified heats
- Key specifications
- • NACE TM0284 / TM0177
IGC (stainless)
Intergranular corrosion test where specified on welded lots
- Key specifications
- • ASTM A262 / ISO 3651
PMI (alloy)
XRF / OES identity check on every alloy heat
- Key specifications
- • API RP 578 practice
Hydro & NDT
Hydro per B31.3 (1.5×); RT/UT on welds per line class
- Key specifications
- • ASME B31.3 §345 / §341
Standards & Certification Map
A complete chemical-pipe specification is a stack of standards — from product spec through alloy class, sour rules, design code and documentation. The five columns below are the ones our mill & engineering team reach for first; project-specific clauses are added on top.
Carbon & alloy product
- ASTM A106 B / C — Seamless carbon steel, high temperature
- ASTM A333 Gr.6 — Low-temperature carbon steel
- ASTM A335 P5–P91 — Seamless Cr-Mo alloy pipe
- EN 10216-2 / -4 — European pressure steel tubes
Stainless & CRA
- ASTM A312 — Seamless & welded austenitic pipe
- ASTM A790 S31803 / S32750 — Duplex & super duplex pipe
- ASTM B423 N08825 — Nickel-iron-chromium alloy 825
- EN 10216-5 — Stainless tubes for pressure
Sour & corrosion
- NACE MR0175 / ISO 15156 — Sour service material limits
- NACE TM0284 — HIC test method
- NACE TM0177 — SSC test method
- API 583 — CUI management
Design & welding
- ASME B31.3 — Process piping design & test
- EN 13480 + PED — EU industrial piping & CE
- ASME IX / ISO 15614 — Welding qualification
- ISO 12944 — Atmospheric corrosion protection
Testing & docs
- ASTM A370 / A751 — Mechanical & chemical test methods
- ASTM A262 / ISO 3651 — IGC test methods
- API RP 578 — PMI guideline
- EN 10204 3.1 / 3.2 — Mill test certificate
Frequently Asked Questions
Six questions we hear most often from process engineers, piping leads and procurement teams.
Which material class does my line need?
The line list decides, but the shorthand holds: carbon steel wherever it survives with a sensible corrosion allowance, 316L where chlorides or cleanliness rule out carbon, duplex where chlorides rule out 316L, nickel alloys where temperature plus chemistry rule out everything cheaper.
What does NACE MR0175 compliance actually mean?
It is condition-dependent, not a stamp: the steel must meet the hardness cap (≤22 HRC) and, on qualified heats, pass HIC testing per NACE TM0284 and SSC testing per TM0177 for the actual H2S partial pressure and pH of your service. Send us both values with the RFQ.
When do I need seamless instead of welded pipe?
Most process line classes below a defined severity prefer welded for cost, but small-bore critical service, very high pressure and many alloy lines specify seamless — A106, A335, A312 are seamless product standards by design.
What is CUI and why does it matter to me?
Corrosion under insulation: water entering lagging corrodes insulated carbon-steel lines between 50 and 175 °C, hidden until failure. The fix is proper coating under insulation (TSA or high-build epoxy), sealed cladding and inspection ports.
What special tests should I expect on alloy pipe?
Impact tests at minimum design temperature (A333 to -46 °C), IGC on welded stainless where specified, PMI on every alloy heat, and hardness surveys after PWHT on Cr-Mo. Anything the line list does not call out, we will not charge you for.
What documentation comes with a chemical-pipe delivery?
EN 10204 3.1 mill certificate as standard, third-party 3.2 on request, heat-number traceability, HIC/SSC reports for sour heats, PWHT and hardness records for alloy, and PMI certificates where applicable.
304L or 316L for a coastal plant?
If the environment involves marine atmosphere or any appreciable chloride in the fluid, 316L — the 2% molybdenum lifts PREN from about 18 to 24 and is the standard defence against coastal pitting. 304L remains fine for inland utility lines. Where chlorides get hot or concentrated, move up to 2205 duplex rather than pushing 316L past its ceiling.
What is pickling and passivation — and do I need it?
Pickling removes weld heat-tint and embedded iron with acid; passivation (e.g. per ASTM A967) rebuilds the protective chromium-oxide film. Pipe that skips this stage starts life with a compromised film exactly at the welds. We deliver stainless pickled and passivated as standard, with certification on request.
How do I actually use the B31.3 wall-thickness formula?
The pressure wall comes from t = P·D / 2(SE + PY): P is design pressure, D outside diameter, S the allowable stress from B31.3 Table A-1, E the weld joint factor (1.0 for seamless), and Y the coefficient that accounts for the nonlinear spread of stress through the wall. That gives the minimum code wall — the corrosion allowance is then added on top, never folded into the formula. Send us the line-list pressure and we size the final wall.
Why does alloy pipe cost roughly double at each step?
The material ladder steps up about two-fold per class: carbon steel → Cr-Mo → austenitic stainless → duplex → nickel alloy. The jump pays for alloy content, tighter melting and inspection, qualified heat treatment, and longer mill lead times — not just the metal. Over-specifying is as expensive as under-specifying, so the line list — not a safety margin — should set the class.
What is the difference between EN 10204 3.1 and 3.2?
Both are material certificates; the difference is who witnesses the tests. A 3.1 is issued by the manufacturer based on its own documented inspection. A 3.2 adds a third-party representative — usually a notified body or your inspector — who is present at testing and signs the certificate. Sour-service, high-pressure and European PED-marked lines commonly call for 3.2; we supply 3.1 as standard and 3.2 on request.
Can you supply to both ASME and EN standards?
Yes. Our mill group covers the ASTM/ASTM range (A106, A333, A335, A312, A790, B423) and the EN 10216 equivalents (P235GH, 16Mo3, 13CrMo4-5, 1.4307/1.4404, 1.4462) from one quality system, so a project can mix ASME B31.3 design with EN 10216 materials, or run fully European (EN 13480 + PED). Dual-certified heats are available where the specification needs both.
Why Buyers Choose CREATEEL for Chemical Pipe
Material ladder + sour competence + code-ready docs, from one mill.
Full material ladder, one source
Carbon, Cr-Mo, stainless, duplex and nickel-alloy pipe from one mill group — no chasing five stockists for five line classes.
Sour-service competence
NACE MR0175 / ISO 15156 supply with HIC (TM0284) and SSC (TM0177) tested heats and hardness certificates — the chemistry other suppliers decline.
Weld-ready alloy packages
Preheat / PWHT schedules, hardness surveys and PMI records ship with the pipe, so site welding starts without surprises.
CUI-aware protection
Coatings selected for the insulated service band — TSA and high-build epoxy options per API 583 practice, holiday-tested before shipment.
Code-ready documentation
ASME B31.3 / EN 13480 + PED referenced on every datasheet, with weld procedures qualified to ASME IX / ISO 15614.
Traceable, audit-proof
EN 10204 3.1 certificate, third-party 3.2 on request, full heat-number trace for the whole delivery — built for turnaround audits.
Related CREATEEL Products
Every chemical project is backed by the mill’s wider steel-pipe catalogue.

Seamless Pressure Pipe
Seamless pressure pipe to ASTM A106 Gr.B and A335 — main steam, feedwater and process headers.
View product details →
Alloy Seamless Pipe
Creep-resistant Cr-Mo grades — T11 / T22 / T91 tube and P5 / P11 / P22 / P91 pipe.
View product details →
Low-Temperature Seamless Pipe
ASTM A333 Gr.6 seamless pipe for cryogenic and low-temperature duty to –45 °C.
View product details →
Seamless Steel Pipe
The full seamless range — hot-finished and cold-drawn, EN 10204 3.1 / 3.2 certified.
View product details →
ERW Steel Pipe
HFW tubing ½″–24″ — utility, offsite and terminal service lines.
View product details →
Steel Flanges
Flanges to ASME B16.5 / B16.47 — weld-neck, slip-on and blind, class 150–2500.
View product details →Ready to Specify Chemical Pipe?
Send us the line list, the H2S / chloride conditions and the codes — we will come back with a mill-direct quote, the material-class proposal and the test / certificate scope the specification calls for.