
Steel Pipe for Fire Protection Systems
Sprinkler, standpipe and deluge networks built on mill-certified steel — ASTM A795 / A53 / A135, EN 10255, GB/T 3091, manufactured against UL 852 and NFPA 13, with the MTC and marking your AHJ expects.
Pipe That Has to Survive the Fire It Fights
An engineering reference for sprinkler contractors, distributors and EPC procurement teams.
Fire-protection pipe has one job nothing else on site can do: stay intact under heat, pressure and water hammer long enough to put the fire out. That is why AHJs, FM and UL auditors treat sprinkler pipe as a life-safety product, not commodity steel — and why the specification you quote has to name the standard, the schedule, the finish and the listing, all at once.
CREATEEL supplies ERW, seamless and galvanized pipe produced specifically for fire-protection duty: ASTM A795 (the fire-specific spec), A53 and A135 for North America, EN 10255 S195T for European projects, GB/T 3091 for China-domestic supply — every length hydrostatically tested, marked per A795 §21 and shipped with an EN 10204 3.1 mill test certificate.
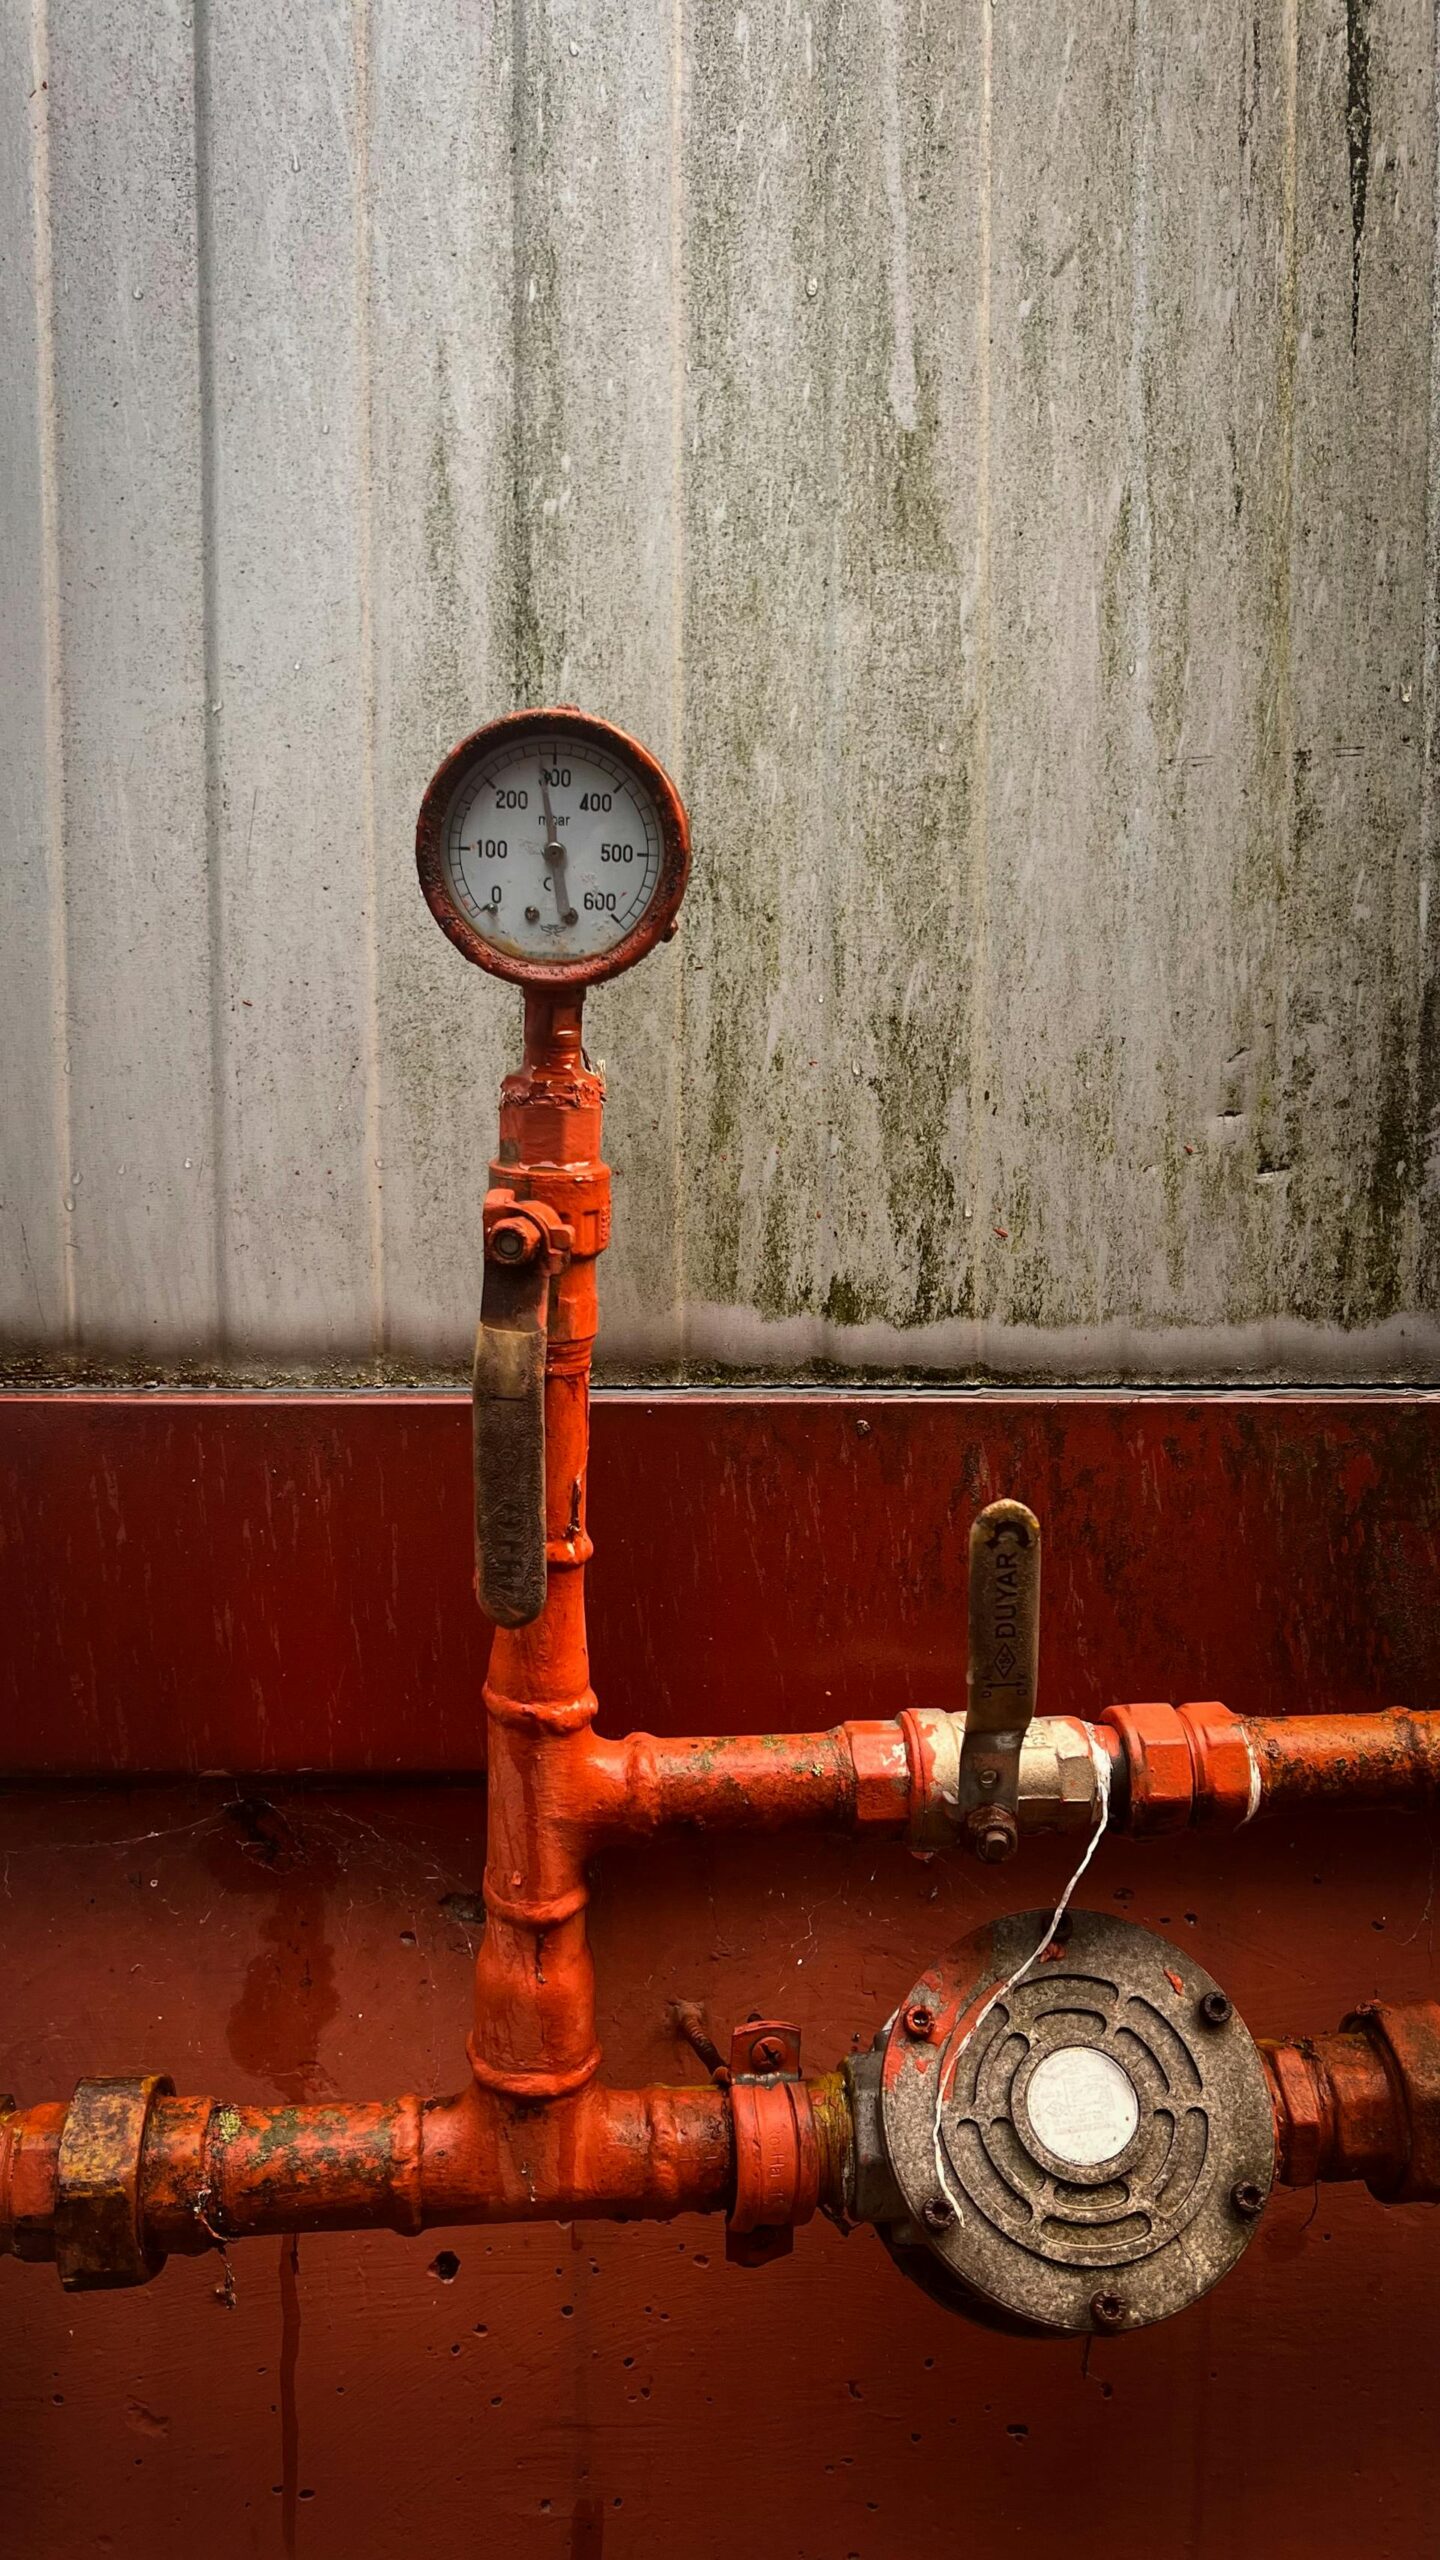
Wet-pipe sprinkler riser with main drain and pressure gauge — the pipe section this page is about.
Four System Architectures, One Pipe Family
The system architecture — not personal preference — decides the schedule and the finish. Wet-pipe grids in conditioned space run light-wall black steel; dry and preaction systems need galvanized pipe to resist internal condensation corrosion; deluge systems on high-hazard occupancies run heavier Schedule 40 walls at higher pressures.
Four system architectures
Wet, dry, preaction and deluge systems place different demands on the same steel tube.
Pipe Types — the ASTM A795 Classification
ASTM A795 classifies fire-protection pipe into three manufacturing types, each with its own size range, chemical requirements and mill hydrotest pressure. Type E (ERW) is the workhorse of modern sprinkler systems; Type F is the low-cost legacy option capped at NPS 4; Type S (seamless) serves high-rise standpipes and offshore modules.
| Type | Process | Size range | Typical use | Mill hydrotest (UL 852) |
|---|---|---|---|---|
| Type F | Furnace-butt welded (continuous welded) | NPS 1/2 – 4 | Cost-driven light-hazard work, legacy systems | 700 psig ≤ NPS 1 · 1200 psig ≥ 1-1/4 |
| Type E | Electric-resistance welded (ERW / HFI) | NPS 1/2 – 10 | The default for wet / dry / preaction sprinkler grids | 1200 psig, ≥ 5 s |
| Type S | Seamless (hot-finished or cold-drawn) | NPS 1/2 – 10 | High-rise standpipes, offshore, high-pressure mains | 1200 psig, ≥ 5 s |
Wall Schedules & System Selection
Schedule selection is a balance of hydraulics, corrosion allowance and listing. Light-weight Sch 10 wall dominates wet-pipe sprinkler grids because it passes the UL 852 fire test; standard-weight Sch 30 / 40 carries threading, standpipe abuse, deluge and dry-system pressures. Where the wall is thinner than Sch 40 (threaded) or Sch 10 (non-threaded), UL 852 requires the pipe to carry its CRR (Corrosion Resistance Ratio) marking: CRR = (X / X40)³.
ASTM A795 wall schedules — light-weight (Sch 10) and standard-weight (Sch 30 / 40)
Nominal wall and mill test pressure per A795 Tables 1–2. Wall tolerance −12.5 % of nominal; weight tolerance ± 5 %.
| NPS | OD (mm) | Light-weight Sch 10 (mm) | Standard-weight Sch 30 / 40 (mm) | Mill test — ERW / S (psig) | Mill test — Type F (psig) |
|---|---|---|---|---|---|
| 1/2″ | 21.3 | — | 2.77 | 700 | 700 |
| 3/4″ | 26.7 | 2.11 | 2.87 | 700 | 500 |
| 1″ | 33.4 | 2.77 | 3.38 | 700 | 500 |
| 1-1/4″ | 42.2 | 2.77 | 3.56 | 1000 | 500 |
| 1-1/2″ | 48.3 | 2.77 | 3.68 | 1000 | 500 |
| 2″ | 60.3 | 2.77 | 3.91 | 1000 | 500 |
| 2-1/2″ | 73.0 | 3.05 | 5.16 | 1000 | 500 |
| 3″ | 88.9 | 3.05 | 5.49 | 1000 | 500 |
| 3-1/2″ | 101.6 | 3.05 | 5.74 | 1200 | 500 |
| 4″ | 114.3 | 3.05 | 6.02 | 1200 | 500 |
| 5″ | 141.3 | 3.40 | 6.55 | 1200 | — |
| 6″ | 168.3 | 3.40 | 7.11 | 1000 | — |
| 8″ | 219.1 | 4.78 † | 7.04 (Sch 30) | 800 | — |
| 10″ | 273.1 | 4.78 † | 7.80 (Sch 30) | 700 | — |
Sch 10 = Schedule 10S of ASME B36.19 for NPS 3/4–6 only. † NPS 8 and 10 light-weight is 4.78 mm (0.188 in.) — not a Schedule 10 wall. Standard-weight is Sch 40 for NPS 1/2–6 and Sch 30 for NPS 8–10. Type F (furnace-welded) pipe is not made above NPS 4. A795 covers NPS 1/2–10.
Matching the schedule to the system
Common practice under NFPA 13 — the schedule follows the system, not the other way round.
| System / duty | Typical wall | Joining method | Why |
|---|---|---|---|
| Wet-pipe sprinklers, NPS 1–2 | Sch 40 (threaded) or Sch 10 (roll-grooved / welded) | Threaded or grooved | Threads need the full Sch 40 wall; grooving allows light wall |
| Wet-pipe sprinklers, NPS 2½–6 | Sch 10 | Grooved or welded | Hydraulically calculated systems rarely need Sch 40 |
| Dry and preaction systems | Sch 40, or Sch 10 with corrosion management | Grooved | Trapped air and sloped piping accelerate corrosion; thicker wall or nitrogen inertion extends life |
| Standpipes and hose stations | Sch 40 minimum | Welded or grooved | Fire-service abuse and FDC surge loading |
| Underground fire loop (NFPA 24) | Ductile iron or lined / 3PE steel | Mechanical restraints | Buried mains follow AWWA practice, not NFPA schedules |
Nominal walls above are what ASTM A795 Tables 1–2 are written against, and what the mill MTC is checked against. A795 permits other wall thicknesses provided every other requirement is still met — but a “Sch 5”, “Sch 7” or “Sch 80” wall is not in Tables 1–2, so it has to be qualified by the listing holder before it can carry a UL / FM mark.
Manufacturing Route — What the Auditor Sees
Nearly all modern sprinkler pipe is electric-resistance welded from hot-rolled coil. For Grade B, A795 requires the weld seam to be heat treated to at least 540 °C so no untempered martensite remains — one of the quiet differences between fire pipe and generic structural tube.
From hot-rolled coil to fire-rated pipe
The ERW line stations a UL 852 / FM audit will walk through.
Grade A vs Grade B — When You Actually Need B
Grades A and B appear in both A53 and A795 for Type E and Type S pipe. Both pass the same hydrostatic test, but Grade B carries higher strength and the mandatory weld-seam heat treatment — which is why NFPA-based high-rise and FM data-sheet specifications quietly assume Grade B.
| Property | Grade A | Grade B |
|---|---|---|
| Yield strength (min) | 205 MPa (30 ksi) | 240 MPa (35 ksi) |
| Tensile strength (min) | 330 MPa (48 ksi) | 415 MPa (60 ksi) |
| Carbon (max) | 0.25 % | 0.30 % |
| Manganese (max) | 0.95 % | 1.20 % |
| Phosphorus / Sulfur (max) | 0.035 % each | 0.035 % each |
| Weld seam heat treatment | Not required | ≥ 540 °C — no untempered martensite (A795 §6.3) |
| Typical duty | Light-hazard residential and light commercial | High-rise, industrial, deluge, standpipe, FM / UL heavy |
Galvanized, Black, FBE or Red — Picking the Skin
Wet-pipe systems live in oxygenated, often stagnant water; dry-pipe systems breathe humid air and collect condensate. The finish decides whether the grid is still clean at year 25 or already tuberculated at year 12.
Hot-dip galvanized
Zinc coating inside and outside by the hot-dip process per A795 §11. Zinc mass ≥ 1.5 oz/ft² (0.46 kg/m²) average, ≥ 1.3 oz/ft² on any single specimen (A90 strip test).
- Key specifications
- • Mandatory practice for dry-pipe systems
- • Parking structures, exposed risers, outdoor
- • Pairs with approved thread sealants
Black steel + sealants
Mill varnish or red-oxide primer over bare steel. Standard for concealed wet-pipe grids in conditioned space where corrosion stress is low and cost matters.
- Key specifications
- • Cheapest installed system
- • Concealed ceilings, riser rooms
- • Microbiologically-influenced corrosion (MIC) risk in stagnant wet systems — ask about nitrogen inerting
FBE coated
Fusion-bonded epoxy, single or dual layer (AWWA C213 / CSA Z245.20 family), 12–16 mil typical. Applied over blasted steel for buried fire mains and aggressive atmospheres.
- Key specifications
- • Buried yard mains and fire loops
- • Offshore modules, chemical plants
- • Holiday-tested ≤ 1 pin per length
Red painted / RAL 3000
Red-oxide or full RAL 3000 paint for exposed sprinkler risers and identification. An identification finish — not a corrosion barrier — always applied over black or galvanized pipe.
- Key specifications
- • Exposed warehouse and atrium risers
- • Fire-service connection tagging
- • FM-recognised colour coding
Coating systems — what is actually measured
The numbers a mill MTC or coating certificate is expected to quote back to you.
| Finish | Governing spec / test | Quantified requirement | Where it belongs |
|---|---|---|---|
| Hot-dip galvanized | A795 §11.2 · ASTM A90 stripping test | Zinc ≥ 1.5 oz/ft² (0.46 kg/m²) average of two 4 in. (102 mm) specimens, and ≥ 1.3 oz/ft² on either one — measured inside + outside, i.e. ≈ 64 µm per surface | Dry, preaction and deluge pipe; exposed risers; parking decks |
| Galvanized with UL / ULC mark | Listing-holder requirement on top of A795 | Coating raised to ≥ 1.8 oz/ft² (≈ 77 µm per surface) before the mark is applied | Any length shipped carrying a UL / ULC listing mark |
| Black — mill varnish / red-oxide primer | Manufacturer standard | ~ 1 mil (25 µm) temporary film — no corrosion allowance, no CRR credit | Concealed wet-pipe grids in conditioned space |
| FBE (fusion-bonded epoxy) | AWWA C213 / CSA Z245.20 family | DFT 12–16 mil (300–400 µm); holiday test ≤ 1 pin per length | Buried fire mains, aggressive soils, plant environments |
| Red painted / RAL 3000 | Identification finish | Nominal 1–2 mil DFT — colour coding only, never a corrosion barrier | Exposed risers, FDC tagging, FM colour code |
Threaded, Grooved, Welded, Flanged
Each joining method has its own standard, tooling and allowance under NFPA 13 and EN 12845. Light-weight pipe may only be roll-grooved, welded or fitted plain-end; standard-weight pipe adds cut groove and threading (A795 §1.2).
| Method | Standard | Typical use | Notes |
|---|---|---|---|
| Threaded (NPT) | ASME B1.20.1 | NPS ≤ 2 standard-weight, light-hazard | Couplings per ASTM A865; sealant must be listed for fire service |
| Roll-grooved | AWWA C606 + listed coupling | All sizes of wet-pipe grids — the modern default | Only method allowed on light-weight pipe; accommodates deflection & expansion |
| Cut-grooved | AWWA C606 | Standard-weight pipe, larger bore, on-site grooving | Removes more wall than roll groove — check remaining wall against CRR |
| Butt-weld | ASME B31.1 / AWS D1.1 | Risers, headers, high-pressure mains | Qualified WPS / PQR and welder continuity records |
| Flanged | ASME B16.5 / EN 1092-1 | Pumps, valves, backflow preventers | Gasket material matched to the medium (EPDM for water, nitrile for foam) |
Rated Pressure, Factory Hydrotest, Site Tests
UL 852 sets the rated working pressure floor; the factory hydrotest is the quality gate every length passes before it ships. Site tests are a different animal — NFPA 13 defines them, and they are the ones your installing contractor cares about.
| Item | Requirement |
|---|---|
| UL 852 rated working pressure (minimum) | ≥ 175 psi (12.1 bar) |
| UL / FM factory hydrotest — ERW & seamless | 1200 psig (83 bar), held ≥ 5 s, every length (or eddy current per ASTM E309) |
| UL / FM factory hydrotest — furnace-welded ≤ NPS 1 | 700 psig (48 bar), ≥ 1 s |
| UL / FM factory hydrotest — furnace-welded ≥ NPS 1-1/4 | 1200 psig (83 bar), ≥ 1 s |
| ASTM A795 mill hydrotest | 500–1200 psi by size and type (Tables 1–2); NDT per E213 / E309 / E570 accepted as alternative |
| NFPA 13 new-system site test | 200 psi (13.8 bar) hydrostatic, 2 h, no leakage |
| NFPA 13 dry / preaction air test | 40 psi (2.8 bar), 24 h, ≤ 1.5 psi drop |
Which Standard Goes Where
A frequent sourcing error is asking for “ASTM A53” when the project actually needs the fire-protection variant. This map shows which material standard, approval mark and installation code line up in each region we ship to.
| Region | Material standard | Approval mark | Installation code |
|---|---|---|---|
| USA & Canada | ASTM A795 (Type E / S, Gr A / B) · ASTM A53 Type E Gr A · ASTM A135 | UL 852 Listed, FM Approved | NFPA 13 / 13R / 13D · NFPA 14 |
| Europe & UK | EN 10255 S195T (Medium / Heavy) · EN 10217-1 P195 / P235 | CE marking where in scope, FM on request | EN 12845 · BS 9251 · BS 5306-2 |
| Middle East / SE Asia | ASTM A795 (most common) · EN 10255 · API 5L PSL1 / PSL2 | FM Approved, third-party witness | NFPA 13 + local civil defence rules |
| China domestic | GB/T 3091 (Q195 / Q215 / Q235B, galvanized) · GB/T 13793 | CCC; FM on request | GB 50016 · GB 50067 · GB 50261 |
| Australia / NZ | AS 1074 ordinary-service steel tubes | SAI Global / third party | AS 2118 series |
Marks, CRR Values and the MTC Chain
Fire-protection pipe is one of the few products where the marking on the pipe is itself a compliance item. The four documents below are what an AHJ, FM field engineer or insurer will ask for first.
Pipe marking (A795 §21)
Every length is stencilled or ink-jetted with the manufacturer name or brand, kind of pipe (continuous-welded, ERW A/B, seamless A/B), ASTM designation and length. NPS 1-1/2 and under may be bundle-tagged.
- Key specifications
- • “NH” letters if not hydrostatically tested
- • Bar coding acceptable as supplement
UL 852 Listed mark
UL certification mark plus the CRR value when the wall is thinner than Sch 40 (threaded) or Sch 10 (non-threaded). CRR = (X / X40)³ per UL 852 §5 and §19.
- Key specifications
- • Verified through UL Follow-Up Services
- • CRR marked on the pipe surface
FM Approved diamond
FM Approvals diamond with size range, schedule and pressure rating, covering wet, dry, preaction and deluge service per the FM data sheets.
- Key specifications
- • Sch 10 / 30 / 40 / 80, NPS 1–12
- • Bending-moment, vibration & fire tested
Mill test certificate — EN 10204 3.1
Heat number, chemistry, tensile results, hydrostatic and NDT records, zinc coating mass where galvanized. Issued per heat and size; the first document every inspector requests.
- Key specifications
- • 3.2 third-party witness on request
- • Retained 10 years at the mill
Frequently Asked Questions
Is ASTM A53 Type E acceptable for a wet-pipe sprinkler system?+
Yes for light- and ordinary-hazard occupancies where the listing allows A53. A795 is the fire-specific specification and the safer call on any project with an FM, UL or insurer review: it adds the light-wall schedules, the fire-end-use marking and tighter hydrotest logic.
What is CRR and when is it marked?+
Corrosion Resistance Ratio — UL 852’s way of comparing a light-wall pipe’s corrosion life to Sch 40: CRR = (X / X40)³. Any threaded pipe thinner than Sch 40, or non-threaded pipe thinner than Sch 10, must carry the CRR value on its surface.
Can you supply UL 852-listed light-wall pipe in galvanized finish?+
Yes. light-wall Sch 10 ERW pipe is supplied black, hot-dip galvanized or red-painted, with the UL listing and CRR marking intact through the galvanizing subcontractor audit.
Do you supply EN 10255 with FM Approval?+
Yes — EN 10255 S195T Medium and Heavy in NPS 1/2–6 with FM Approval certificates, the combination most European FM-scheme projects ask for.
What is the lead time for, say, 500 t of A795 Sch 10 NPS 2 galvanized?+
Typically 30–45 days FOB Tianjin including the listing audit; heavier schedules, seamless Types and 3.2 MTC witnesses add 15–25 days. Send the size range for a mill-direct quote.
UL Listed vs FM Approved — do I need both?+
They are separate certification bodies: UL (Underwriters Laboratories) and FM (FM Approvals). Most US authorities accept either, but some FM-insured plants write FM Approval into the specification. Tell us which one your AHJ or insurer requires — the steel is the same, the certification paperwork differs.
What wall do I need for roll-grooved joints?+
Roll grooving cold-forms the groove and displaces metal, so it needs light-wall pipe with enough ductility — exactly what A795 Sch 10 is made for. Cut grooves remove metal and suit heavier schedules. Never roll-groove pipe above the manufacturer’s groove-wall limit.
Standards & Certification Map
Fire-protection pipe is one of the few product lines where the standard matters more than the brand — the AHJ approves the standard, not the catalogue. These are the specifications CREATEEL manufactures and certifies against.
US fire-pipe standards
- ASTM A795 / A795M — Black & galvanized welded and seamless pipe for fire protection — Type F / E / S, Gr A / B
- ASTM A53 / A53M — Type E Gr A — the ERW feedstock accepted by UL 852 sprinkler grids
- ASTM A135 / A135M — ERW pipe Gr A / B — approved stock under UL 852
- UL 852 — Metallic sprinkler pipe — bending moment, vibration, leak, hydrotest and fire test regime
- FM Approvals — Factory Mutual Approved, Sch 10 / 30 / 40 / 80, NPS 1–12
- NFPA 13 / 13R / 13D / 14 — Sprinkler, residential and standpipe installation codes
International standards
- EN 10255 — S195T, Light / Medium / Heavy — the European fire-pipe default (ex BS 1387)
- ISO 65 — Carbon steel tubes for threading — international EN 10255 counterpart
- EN 10217-1 — Welded pressure tubes — P195 / P235 / P265 for higher-pressure fire mains
- GB/T 3091 — Q195 / Q215 / Q235B, galvanized option — China domestic sprinkler pipe
- GB/T 13793 — ERW pipe for low / medium pressure — basis of China-made UL listings
- AS 1074 — Ordinary-service steel tubes — Australia / NZ fire grids
Quality & documentation
- EN 10204 3.1 / 3.2 — Mill test certificate, third-party witness option
- ASTM E213 / E309 / E570 — Ultrasonic, eddy-current and flux-leakage NDT alternatives to hydrotest
- ASTM A90 — Zinc coating mass strip test
- ASME B1.20.1 — NPT thread gauging practice
- AWWA C606 — Grooved and shouldered joints
- ISO 9001 — Mill quality system
Related CREATEEL Products
Fire-protection pipe is rarely specified alone — these are the lines that usually share the same MTC and shipment.

ERW Steel Pipe
HFW pipe 1/2″–24″ to ASTM A53 / A795 / API 5L / EN 10255 — the base material of sprinkler grids.
View product details →
Seamless Steel Pipe
Hot-finished seamless to ASTM A53 Type S / A106 for high-pressure mains and standpipes.
View product details →
LSAW Steel Pipe
UOE / JCOE large-diameter pipe for fire-water mains, tank connected loops and plant fire networks.
View product details →
3PE Coated Pipe
Three-layer polyethylene per ISO 21809-1 / DIN 30670 for buried fire-water mains.
View product details →
FBE Coated Pipe
Single / dual-layer FBE per AWWA C213 / CSA Z245.20 for aggressive soils and plant environments.
View product details →
Galvanized Steel Pipe
Hot-dip galvanized pipe to ASTM A53 / EN 10255 — the proven sprinkler and standpipe material.
View product details →Ready to Specify Fire-Protection Pipe?
Send the standard, schedule, finish and certification you need — ASTM A795, EN 10255, GB/T 3091, UL 852 or FM — and our fire-protection engineers will come back with a mill-direct quote and a sample MTC within one business day.

 +86 15602135951 |
 WhatsApp Available